
Threaded Insert Drilling Depth (UNC Threads)
Per-thread drilling data for threaded insert installations in the UNC coarse series from 2-56 through 1/2-13 — tap drill diameter, drilled-hole diameter limits, tap minimum outer diameter, and drilling depth for insert engagements from 1d to 3d.
Last updated: 2026-11
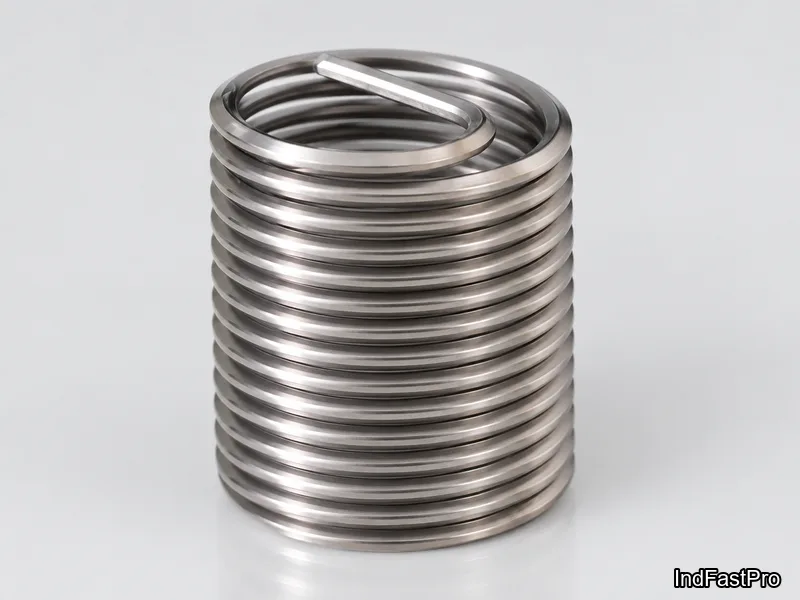
Specifications
The inch-series companion to the metric drilling-depth chart: for each UNC coarse designation from the small 2-56 up to 1/2-13, this table gives the drill bit diameter for the pre-tap hole, the minimum and maximum drilled diameter, the tap minimum outer diameter, and the drilling depth needed for insert engagements of 1d, 1.5d, 2d, 2.5d and 3d, with d the nominal major diameter. The source prints pitch in millimetres even on the inch designations (2-56 at 0.453 mm, 1/4-20 at 1.270 mm) — carry the pitch unit with you when checking against a tap label marked in TPI. The engagement ladder starts at 1d on this chart (the source does not tabulate 0.5d or 0.75d for UNC), which matches how inch-series inserts are actually applied — sub-1d engagement is rare in the UNC world. Use it the same way as the metric chart: pick the engagement your joint needs, read the depth at your designation, and mind the bottom-clearance margin on blind holes. Insert length selection and parent-material corrections are per RFQ.
| Coverage | 22 UNC coarse designations, 2-56 through 1/2-13 (thread numbers 2-56, 3-48, 4-40, 5-40, 6-32, 8-32, 10-24, 10-32, then 1/4-20 up to 1/2-13) |
|---|---|
| Columns | Pitch (mm); drill bit diameter; drilling diameter min./max.; tap minimum outer diameter; drilling depth at 1d / 1.5d / 2d / 2.5d / 3d engagement — all mm as printed |
| Unit note | Pitch is printed in mm (e.g. 1/4-20 → 1.270); convert to TPI (25.4 / pitch) when matching against inch-labeled taps |
| Engagement range | 1d to 3d — the source tabulates no 0.5d / 0.75d columns for UNC |
| Not tabulated | UNF companions are on their own page; insert lengths, materials — per RFQ |
| Nominal Diameter | Pitch (mm) | Drill Bit Diameter (mm) | Drilling Diameter | Tap | Drilling Depth | |||||
|---|---|---|---|---|---|---|---|---|---|---|
| min. | max. | Min Outer Diameter | 1d | 1.5d | 2d | 2.5d | 3d | |||
| 2-56 | 0.453 | 2.4 | 2.30 | 2.50 | 2.77 | 4.2 | 5.3 | 6.4 | 7.5 | 8.6 |
| 3-48 | 0.529 | 2.7 | 2.65 | 2.80 | 3.20 | 4.9 | 6.2 | 7.4 | 8.7 | 10.0 |
| 4-40 | 0.635 | 3.1 | 3.00 | 3.15 | 3.67 | 5.7 | 7.1 | 8.6 | 10.0 | 11.4 |
| 5-40 | 0.635 | 3.4 | 3.33 | 3.50 | 4.00 | 6 | 7.6 | 9.2 | 10.8 | 12.4 |
| 6-32 | 0.794 | 3.8 | 3.68 | 3.89 | 4.54 | 7.1 | 8.8 | 10.6 | 12.3 | 14.1 |
| 8-32 | 0.794 | 4.4 | 4.34 | 4.52 | 5.20 | 7.7 | 9.8 | 11.9 | 14.0 | 16.1 |
| 10-24 | 1.058 | 5.2 | 5.06 | 5.28 | 6.20 | 9.6 | 12.0 | 14.4 | 16.8 | 19.2 |
| 12-24 | 1.058 | 5.8 | 5.72 | 5.92 | 6.86 | 10.3 | 13.0 | 15.7 | 18.5 | 21.3 |
| 1/4-20 | 1.270 | 6.7 | 6.62 | 6.86 | 8.00 | 12.1 | 15.2 | 18.4 | 21.6 | 24.8 |
| 5/16-18 | 1.411 | 8.4 | 8.24 | 8.49 | 9.77 | 14.3 | 18.3 | 22.2 | 26.2 | 30.2 |
| 3/8-16 | 1.588 | 10.0 | 9.89 | 10.12 | 11.59 | 16.7 | 21.4 | 26.2 | 31.0 | 35.7 |
| 7/16-14 | 1.814 | 11.6 | 11.51 | 11.78 | 13.47 | 19.3 | 24.8 | 30.4 | 35.9 | 41.5 |
| 1/2-13 | 1.954 | 13.2 | 13.12 | 13.40 | 15.24 | 21.5 | 27.8 | 34.2 | 40.5 | 46.9 |
| 9/16-12 | 2.117 | 14.9 | 14.75 | 15.03 | 17.04 | 23.8 | 31.0 | 38.1 | 45.2 | 52.4 |
| 5/8-11 | 2.309 | 16.5 | 16.38 | 16.68 | 18.88 | 26.3 | 34.2 | 42.1 | 50.1 | 58.0 |
| 3/4-10 | 2.540 | 19.8 | 19.60 | 19.91 | 22.35 | 30.5 | 40.0 | 49.5 | 59.0 | 68.6 |
| 7/8-9 | 2.822 | 23.0 | 22.84 | 23.18 | 25.89 | 34.9 | 46.0 | 57.2 | 68.3 | 79.4 |
| 1″-8 | 3.175 | 26.4 | 26.09 | 26.47 | 29.53 | 39.7 | 52.4 | 65.1 | 77.8 | 90.5 |
| 1″ 1/8-7 | 3.629 | 29.5 | 29.36 | 29.74 | 33.29 | 44.9 | 59.2 | 73.5 | 87.8 | 102.0 |
| 1″ 1/4-7 | 3.629 | 32.8 | 32.54 | 32.92 | 36.46 | 48.1 | 64.0 | 79.8 | 96.0 | 111.8 |
| 1″ 3/8-6 | 4.234 | 36.2 | 35.84 | 36.35 | 40.42 | 54.0 | 71.4 | 88.9 | 106.0 | 124.0 |
| 1″ 1/2-6 | 4.234 | 39.5 | 39.02 | 39.53 | 43.62 | 57.2 | 76.2 | 95.3 | 115.0 | 133.0 |
Materials
- Hole sizing is material-independent; the insert is the material decision. Quote the parent material and the UNC callout together on the RFQ — UNC inserts in aluminum castings are a common repair combination and typically take the 1.5d to 2d engagement rows of this chart. Insert supply (free-running vs screw-locking wire series, self-tapping, heavy-duty) across carbon steel, stainless and exotic alloys per the family pages
Ordering & documentation
Documents
Shipments of Threaded Insert Drilling Depth (UNC Threads) are backed by Mill Test Certificate (MTC), Dimensional Report, Salt Spray Test Report on request, with full batch traceability from raw material to finished product. Quality management for Threaded Insert Drilling Depth (UNC Threads) orders follows the owner-confirmed compliance list: ISO 9001:2015, RoHS, REACH. Exact document sets are confirmed on the order.
Quotation
- The product family (Threaded Insert Drilling Depth (UNC Threads)), product standard/designation and drawing or part number.
- The dimensions that apply to this part — such as size, pitch, length, thickness, fit, grip or groove geometry.
- Material/grade, heat-treatment condition and surface finish, together with the service environment.
- Quantity per size, delivery destination and required test or traceability documents.
Sample & supply
Minimum order quantities and lead times for threaded insert drilling depth (unc threads) are confirmed at quotation — send insert type, thread size and installation method on the RFQ and the quote will carry a firm schedule; sample availability is confirmed with the quotation.
Storage & shipping
Threaded Insert Drilling Depth (UNC Threads) are packed for export and shipped factory-direct to buyers in Europe, Asia, the Americas and the Middle East. Store threaded insert drilling depth (unc threads) dry and protected until installation, and keep coated parts in their packaging until use; specific packing and preservation requirements can be stated on the order and confirmed at quotation.
Frequently asked questions
Why does the chart print pitch in millimetres for inch threads?
Because the machining numbers are metric: the drill diameters, drilled-hole limits and depths are all in mm, and the source keeps the pitch column in the same unit system so the whole row reads in one system. To sanity-check against a tap labeled 1/4-20, convert: 25.4 divided by 20 TPI gives 1.27 mm, which is the chart's 1/4-20 pitch. The depth columns convert the same way if your drawing is inch-denominated (25.4 mm to the inch). What you should not do is mix a metric tap with the chart's UNC drill column — the drill diameters tabulated here are matched to the UNC thread form's minor diameter, and a metric-designation tap of similar size will cut a different thread entirely. Match designation to designation, then read the row.
My drawing calls a 10-32 insert but the chart shows both 10-24 and 10-32. Which row governs the drilling?
The 10-32 row — the second number is the thread count and it changes everything downstream of the pilot hole: 10-24 (24 TPI, pitch 1.058 mm) and 10-32 (32 TPI, pitch 0.794 mm) take different tap drills, and their drilled-diameter limits do not interchange. This is the most common transcription error in insert work because the nominal (No. 10) is identical. Read the full designation from the drawing, find it verbatim in the chart's first column, and take the whole row from that line. If your drawing has an unresolved conflict between the insert callout and the tapped-hole callout, resolve it before ordering — an insert supplied against the wrong designation is scrap at install.
Request a Quote
Get factory-direct pricing from the manufacturer.
What to include in your Threaded Insert Drilling Depth (UNC Threads) inquiry
- ✓ Identify insert type (helical/tangless, solid, self-tapping, key-locking, heat-set or rivet nut) and internal thread.
- ✓ Give insert length, parent-material type/hardness, available wall thickness and hole dimensions.
- ✓ State installation method and tooling, including tapping or prepared-hole requirements.
- ✓ Describe required pull-out/torque-out resistance, anti-rotation or locking needs and service environment.
- ✓ Factory-direct pricing for your Threaded Insert Drilling Depth (UNC Threads)
- ✓ Standard and custom specifications
- ✓ Factory-direct export to buyers in Europe, Asia, the Americas and the Middle East
- ✓ Full fastener family support