
ISO Class 12.9 Bolts
Property Class 12.9 bolts per ISO 898-1 — high alloy steel, quenched and tempered, 1,220 MPa minimum tensile, 1,100 MPa yield, 39–44 HRC. The highest-strength common metric grade for precision and high-stress applications.
Last updated: 2026-11
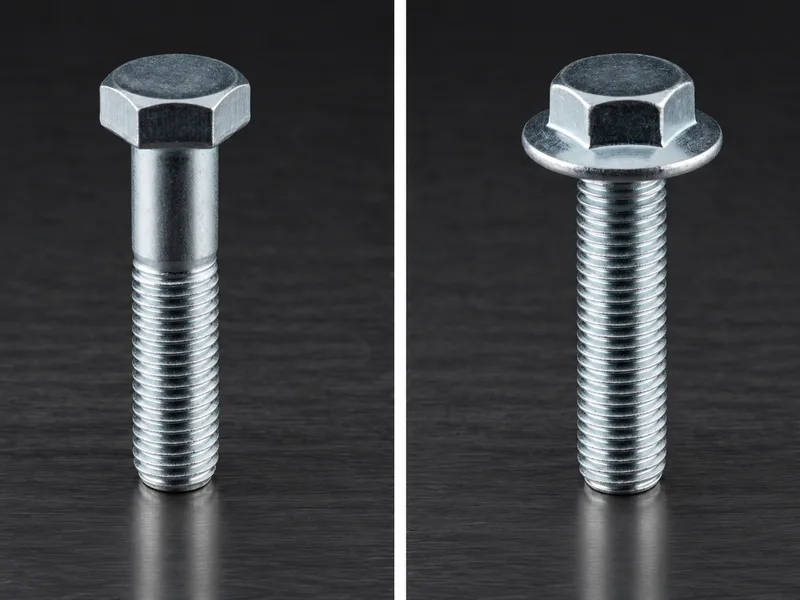
Specifications
Class 12.9 is the top of the common ISO range: quenched and tempered high alloy steel with a minimum tensile of 1,220 MPa and yield at 90% of tensile. It is specified where maximum clamp load in a compact envelope matters — precision machinery, high-stress driveline and tooling applications, and aerospace-adjacent equipment. Above roughly 1,000 MPa material strength, hydrogen embrittlement becomes a real design consideration: electroplated 12.9 parts require strict bake practice, and zinc flake is often chosen precisely to avoid the risk.
| Standard | ISO 898-1, property Class 12.9 (socket head cap screws and hex bolts) |
|---|---|
| Material | High alloy steel, quenched and tempered |
| Tensile strength, min | 1,220 MPa (nominal 1,200 MPa) — 176,900 psi |
| Yield strength (min) / proof load | 1,100 MPa yield; proof load 970 MPa |
| Hardness | 39–44 HRC |
| Hydrogen embrittlement | Sensitive at this strength level — post-plate bake required for electroplated parts; zinc flake avoids the risk |
| Typical applications | Precision machinery, extremely high-stress assemblies, tooling, aerospace components |
Where this grade fits
Above roughly 1000 MPa tensile, hydrogen embrittlement is a real design consideration: avoid hydrogen-sensitive scenarios for this grade, specify zinc flake (ISO 10683) rather than electroplate or hot-dip galvanizing where corrosion protection is needed, and require a documented bake whenever electroplating is unavoidable. The full coating-selection logic and bake sequencing are in the coating and embrittlement guides.
Deep read: Zinc-Flake vs Zinc-Nickel for High-Strength Fasteners: What the Evidence Settles on Hydrogen, Salt Spray, Friction and Specs · Hydrogen Embrittlement in High-Strength Bolts: Which Grades Need Controls, Which Coatings and Baking Schedules Are Acceptable, and What to Require Before the RFQ
Materials
- High alloy steel (quenched and tempered)
Class 12.9 must be alloy steel, quenched and tempered, with carbon 0.28-0.50% and a minimum tempering temperature of 380 °C.
ISO 898-1 defines alloy steel strictly — at least one of chromium 0.30%, nickel 0.30%, molybdenum 0.20% or vanadium in the stated amounts — so check the MTR lists one of these elements rather than a plain carbon-manganese analysis.
Ordering & documentation
Documents
Shipments of ISO Class 12.9 Bolts are backed by Mill Test Certificate (MTC), Dimensional Report, Salt Spray Test Report on request, with full batch traceability from raw material to finished product. Quality management for ISO Class 12.9 Bolts orders follows the owner-confirmed compliance list: ISO 9001:2015, RoHS, REACH. Exact document sets are confirmed on the order.
Quotation
- The product family (ISO Class 12.9 Bolts), product standard/designation and drawing or part number.
- The dimensions that apply to this part — such as size, pitch, length, thickness, fit, grip or groove geometry.
- Material/grade, heat-treatment condition and surface finish, together with the service environment.
- Quantity per size, delivery destination and required test or traceability documents.
Sample & supply
Supply source for ISO Class 12.9 Bolts: own manufacturing plus qualified outsourcing (per the owner-confirmed scope of supply (own production plus outsourcing)).
Minimum order quantity for iso class 12.9 bolts is 1,000–10,000 pieces depending on size (applies to the standard sizes and finishes for iso class 12.9 bolts; mixed, special or custom variants are quoted — final commercial terms per quotation) Stock items for iso class 12.9 bolts run 3–7 days. High-strength and custom parts for iso class 12.9 bolts run 15–25 days. Quantities or variants of iso class 12.9 bolts outside the standard range are confirmed at quotation.
Storage & shipping
ISO Class 12.9 Bolts are packed for export and shipped factory-direct to buyers in Europe, Asia, the Americas and the Middle East. Store iso class 12.9 bolts dry and protected until installation, and keep coated parts in their packaging until use; specific packing and preservation requirements can be stated on the order and confirmed at quotation.
Frequently asked questions
Does Class 12.9 tolerate hot-dip galvanizing?
It is not the recommended path. The zinc bath temperature tempers the part and the grade's extreme strength makes any hydrogen pickup from pre-treatment a genuine embrittlement risk. Where a corrosion-protected 12.9 part is needed, zinc flake systems (ISO 10683) or mechanical plating with a qualified bake are the usual specification. Confirm the coating with the drawing — if it calls for 12.9 with HDG, treat it as an engineered exception to be quoted explicitly.
What is the MOQ and lead time for this bolt grade?
The minimum order quantity for ISO Class 12.9 Bolts is 1,000–10,000 pieces depending on size. Stock items of ISO Class 12.9 Bolts ship in 3–7 days; high-strength and custom parts in 15–25 days. Common diameters of ISO Class 12.9 Bolts are widely stocked; confirm the exact schedule against quantity and size mix at quotation.
What should an RFQ for this bolt grade state?
For ISO Class 12.9 Bolts, state the standard and grade (for example ISO 4017 Class 8.8 or ASTM F3125 Grade A325 Type 1), diameter and length, thread type (metric coarse or UNC/UNF), finish (plain, zinc, or hot-dip galvanized where the grade permits), required certificates such as a mill test report per EN 10204 3.1, and quantity per size — plus destination country.
Related knowledge
- What Bolt Property Classes 8.8, 10.9 and 12.9 Encode — and When High Strength Stops Being the Right Choice
- Bolt Grade Selection: ISO 898-1 8.8/10.9/12.9 vs ASTM A307 and A325
- 8.8 vs 10.9 vs 12.9 Bolts: Strength, Hardness and Cost — What the Evidence Settles
- Calculating Bolt Preload and Clamp Force: Torque, Friction and Tightening Method
- How to Determine Tightening Torque and Choose a Tightening Method for a Bolted Joint
- Fastener Failure Modes: Which Fatigue, Creep and SCC Controls the Evidence Supports
- Hydrogen Embrittlement in High-Strength Bolts: Which Grades Need Controls, Which Coatings and Baking Schedules Are Acceptable, and What to Require Before the RFQ
Request a Quote
Get factory-direct pricing from the manufacturer.
What to include in your ISO Class 12.9 Bolts inquiry
- ✓ Name the bolt standard and product form, then give nominal diameter, pitch, length and threaded length.
- ✓ State the applicable property class or material grade, head style, and coating or finish.
- ✓ Identify the mating nut/washer and the joint duty; include any specified preload, tightening method or friction condition.
- ✓ Give quantity per size, destination and required material or inspection certificates.
- ✓ Factory-direct pricing for your ISO Class 12.9 Bolts
- ✓ Standard and custom specifications
- ✓ Factory-direct export to buyers in Europe, Asia, the Americas and the Middle East
- ✓ Full fastener family support